Quick Answer: What Tool Steel Is Best for Glass-Filled Plastics?
Glass-filled plastics are significantly more abrasive than unfilled polymers. Long glass fibers and short glass fibers can accelerate cavity, core, gate and insert wear, especially when the mold operates at high injection pressure and production volume.
For glass-filled plastic injection molds, tool steel should be selected primarily for:
- High abrasive wear resistance
- Adequate toughness and chipping resistance
- High compressive strength
- Good dimensional stability after heat treatment
- Suitable polishability for the required surface finish
- Resistance to erosion around gates, runners and sharp cavity features
- Compatibility with nitriding or PVD coatings when additional wear protection is required
For moderate to high wear applications, high-hardness cold work tool steels such as D2/SKD11-type grades can be considered. For more demanding molds, higher-toughness or premium refined tool steels may provide a better balance between wear resistance and resistance to chipping.
The correct grade depends on the glass-fiber percentage, resin system, mold geometry, production volume, surface finish and actual failure mode.
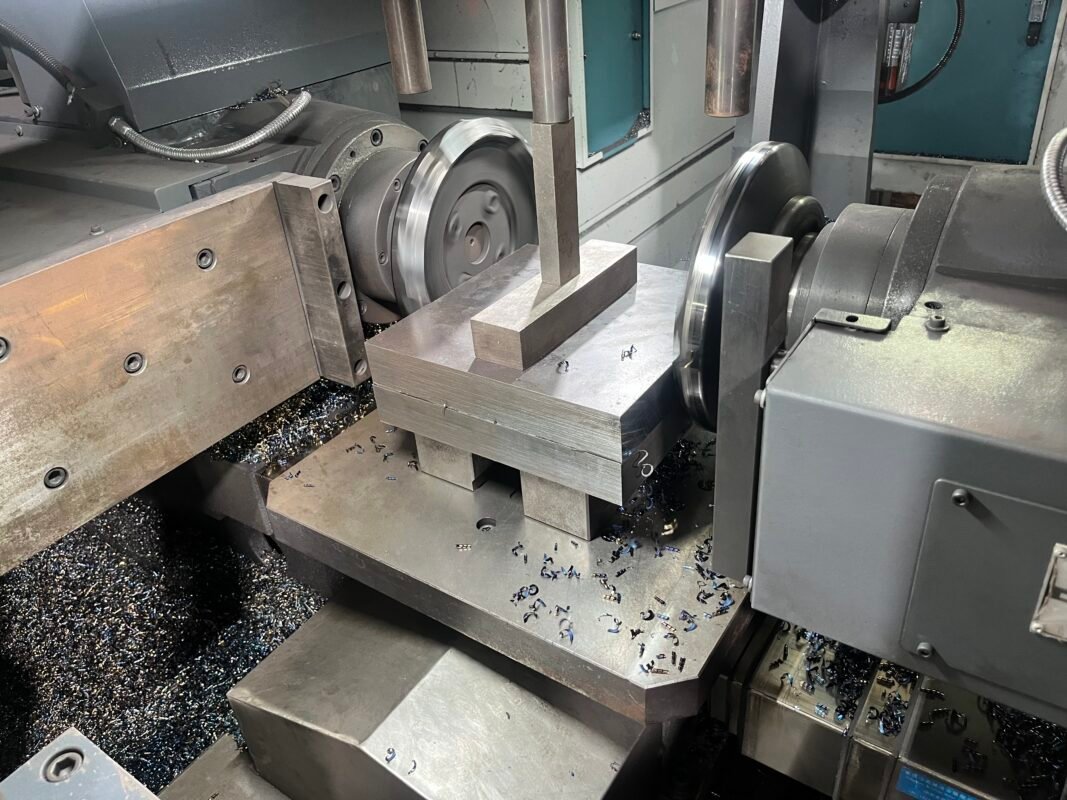
Why Glass-Filled Plastics Cause Cavity Erosion
Glass-filled engineering plastics are widely used in automotive, electrical, electronics, industrial and consumer applications because glass fibers improve stiffness, strength and dimensional stability.
However, these same fibers create a much more aggressive molding environment for the tool steel.
A conventional unfilled polymer generally produces relatively low abrasive wear. Adding glass fiber changes the wear mechanism.
During injection, the polymer melt carries glass fibers through the runner system, gate and cavity. At high velocity and pressure, the fibers repeatedly contact the steel surface.
The result can include:
- Abrasive cavity wear
- Gate erosion
- Runner enlargement
- Loss of sharp edges
- Wear around ribs and bosses
- Polishing or texturing changes
- Parting-line wear
- Dimensional drift
- Surface defects on molded parts
Over thousands or millions of molding cycles, even relatively small amounts of steel removal can become a serious production problem.
Cavity erosion is not always uniform
One of the most important points in mold steel selection is that wear is often concentrated in specific areas.
Typical high-wear locations include:
- Gates
- Runners
- Sharp cavity transitions
- Core pins
- Thin ribs
- Edges and shutoffs
- Areas where glass fibers change direction
- High-flow-velocity regions
Therefore, simply choosing the hardest available steel is not always the best solution.
The mold must be designed around the actual wear mechanism.
Key Tool Steel Requirements for Glass-Filled Injection Molds
1. High Abrasive Wear Resistance
Wear resistance is usually the first material-selection criterion for glass-filled plastic molds.
Glass fibers can act as hard abrasive particles against the cavity surface. The steel must therefore resist material removal during repeated injection cycles.
High-carbon, high-chromium cold work tool steels are commonly considered for wear-intensive applications because their carbide structure can provide strong resistance to abrasive wear.
However, wear resistance must be evaluated together with toughness.
A steel with extremely high carbide content may provide excellent wear resistance but become more susceptible to edge chipping if the mold contains thin sections, sharp corners or heavily loaded shutoffs.
2. Toughness and Chipping Resistance
Cavity erosion is only one possible failure mode.
Glass-filled molds can also experience:
- Edge chipping
- Cracking
- Shutoff damage
- Core breakage
- Insert failure
- Fatigue cracking
This is particularly important for molds containing thin ribs, narrow slides or small core pins.
A practical material-selection strategy is therefore:
Choose the highest wear resistance that the mold geometry and mechanical loading can safely tolerate.
For example, a large cavity insert with relatively thick sections may tolerate a high-wear cold work steel better than a small, thin core pin subjected to impact and bending.
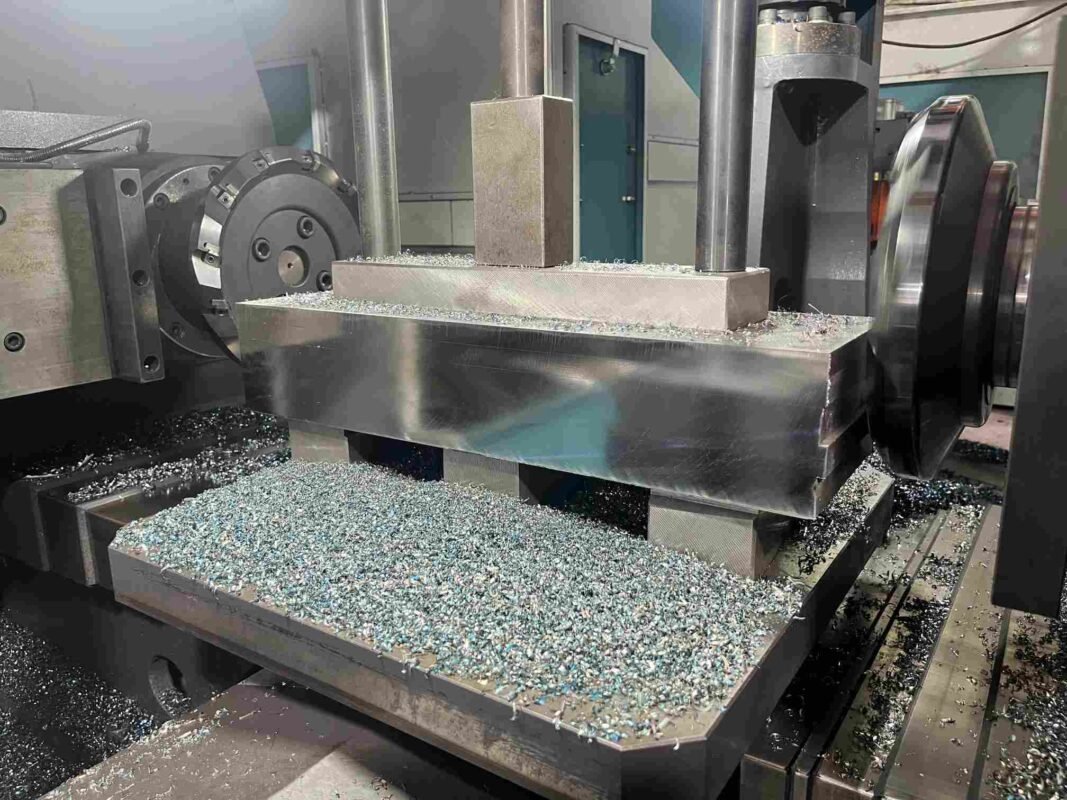
3. Compressive Strength
Injection molding can generate substantial local pressure around:
- Shutoffs
- Slides
- Small cores
- Ribs
- Inserts
- Thin cavity sections
High compressive strength helps the tool steel maintain dimensional integrity under repeated loading.
This becomes particularly important when the glass-filled polymer is highly reinforced and the mold contains precision shutoff areas.
4. Dimensional Stability
A glass-filled plastic mold may be required to maintain tight dimensional tolerances over a very large number of cycles.
Poor dimensional stability can cause:
- Cavity dimensions to drift
- Part dimensions to change
- Flash to develop
- Shutoff fit to deteriorate
- Mold maintenance intervals to decrease
Heat treatment is therefore just as important as the nominal steel grade.
A high-quality tool steel can still produce poor mold performance if hardening, tempering, stress relieving or cryogenic treatment is improperly controlled.
Comparing Common Tool Steel Options
Different mold applications require different balances between wear resistance and toughness.
| Steel Type | Wear Resistance | Toughness | Typical Application |
|---|---|---|---|
| P20 / 718H | Moderate | Good | General plastic molds |
| H13 / SKD61 | Good | High | Hot sections, inserts, moderate wear |
| S136 | Good | Good | Corrosive plastics, polished cavities |
| D2 / SKD11 | Very Good | Moderate | High-wear plastic mold components |
| DC53 | Very Good | Better than traditional D2-type steel | Wear + toughness applications |
| PM Tool Steel | Excellent | Grade-dependent | Severe wear and high-volume tooling |
This table should not be treated as a universal ranking.
The best material depends on the failure mode and mold design.
D2 / SKD11 for Glass-Filled Plastic Molds
D2/SKD11-type cold work tool steel is a common candidate when abrasive wear is the primary concern.
Its high chromium and carbide content provides strong resistance to abrasive wear compared with conventional pre-hardened mold steels.
It can be suitable for:
- High-wear cavity inserts
- Core inserts
- Wear plates
- Mold components exposed to glass-filled compounds
- High-volume molding applications
However, D2/SKD11 is not automatically the best choice for every glass-filled plastic mold.
Its relatively high carbide content can make toughness and edge stability important considerations, particularly for complex geometries or thin sections.
For applications where chipping is a recurring problem, a tougher steel or premium powder-metallurgy grade may be more appropriate.
DC53 for Wear and Toughness Balance
DC53-type tool steel is often considered when conventional D2/SKD11 provides sufficient wear resistance but additional toughness is required.
For molds containing:
- Thin ribs
- Small cores
- Complex inserts
- Precision shutoffs
- Repeated mechanical loading
a better balance between hardness, wear resistance and toughness can be more valuable than simply maximizing hardness.
The objective is not to select the hardest steel.
The objective is to minimize total mold downtime and maintenance.
PM Tool Steel for Severe Glass-Fiber Wear
When glass-fiber abrasion is extremely severe, powder-metallurgy tool steels can become an attractive option.
PM steels can provide a highly controlled carbide structure with a combination of:
- High wear resistance
- High compressive strength
- Good toughness
- Improved carbide distribution
- Better performance in demanding tooling applications
They are particularly relevant when:
- Glass-fiber content is high
- Production volume is very high
- Mold maintenance is expensive
- Dimensional stability is critical
- Conventional cold work steels wear too quickly
The additional material cost should be compared with the total cost of mold maintenance, downtime and replacement inserts.
Why Mold Hardness Alone Does Not Stop Cavity Erosion
A common mistake is to assume:
Higher HRC = longer mold life.
This is not always correct.
Mold performance depends on the interaction between:
Steel grade + carbide structure + heat treatment + surface condition + mold geometry + molding parameters.
For example, excessive hardness without sufficient toughness may increase the risk of chipping.
Similarly, a wear-resistant steel can still experience rapid erosion if the gate design produces excessive melt velocity in a small area.
Therefore, the target hardness should be established based on the selected steel grade and application rather than simply choosing the highest possible hardness.
Gate Design Can Accelerate Mold Erosion
The gate is often one of the first areas to show wear in glass-filled injection molding.
Why?
Because the gate combines:
- High melt velocity
- High pressure
- Abrasive glass fibers
- Repeated thermal cycling
- Concentrated material flow
A poorly designed gate can cause localized erosion even when the cavity steel is properly selected.
For severe applications, consider:
- Replaceable gate inserts
- Wear-resistant inserts
- Appropriate gate dimensions
- Smooth flow transitions
- Reduced unnecessary flow velocity
- Proper gate location
A replaceable insert can sometimes be more economical than manufacturing the entire cavity from an extremely expensive premium steel.
Fiber Orientation and Localized Wear
Glass fibers do not necessarily move through the cavity in a random pattern.
Their orientation is affected by:
- Gate location
- Flow direction
- Cavity geometry
- Flow velocity
- Wall thickness
- Cooling conditions
This can create localized wear patterns.
Sharp changes in flow direction can increase contact between glass fibers and the cavity wall.
For this reason, mold-flow analysis can be useful for high-volume or high-value tooling.
The objective is not only to predict filling and weld lines.
It can also help identify regions where aggressive material flow may contribute to accelerated tool wear.
Surface Treatment for Glass-Filled Plastic Molds
When the base steel has been correctly selected, surface treatment can provide another layer of protection.
Nitriding
Nitriding can increase surface hardness and improve resistance to wear and surface damage.
It may be useful for selected mold components where:
- Surface wear is concentrated
- Dimensional stability is important
- A hard diffusion layer is appropriate
- The substrate has sufficient toughness
The nitriding process must be controlled carefully because excessive compound-layer formation or dimensional changes may be undesirable for precision mold components.
PVD Coatings
PVD coatings such as TiN, CrN, AlTiN and other advanced coating systems can be considered for severe wear environments.
Potential benefits include:
- Increased surface hardness
- Reduced adhesive wear
- Improved resistance to abrasion
- Extended maintenance intervals
However, coating a poorly selected substrate does not solve the fundamental problem.
If the substrate lacks toughness or has poor heat treatment, coating it will not prevent cracking or bulk failure.
The correct approach is:
Select the substrate first, optimize heat treatment second, and use surface treatment to address the remaining wear mechanism.
ESR Tool Steel for High-Wear Injection Mold Components
Steel cleanliness and carbide distribution can become increasingly important as mold performance requirements increase.
Electroslag remelting (ESR) can improve steel cleanliness and provide a more controlled internal structure compared with conventional production routes.
For precision mold components, improved material consistency can contribute to:
- Better polishability
- More predictable heat treatment
- Improved toughness
- Reduced internal defects
- More consistent machining behavior
For high-value glass-filled plastic molds, premium refined tool steel may be justified when mold failure or frequent maintenance carries a significant production cost.
Should You Use One Steel for the Entire Mold?
Not necessarily.
A hybrid mold construction can be more economical.
For example:
General mold body
Use a conventional mold steel such as P20 or 718H where wear is relatively low.
High-wear cavity insert
Use a higher wear-resistant tool steel.
Gate insert
Use a replaceable wear-resistant insert.
Small core pin
Select a steel based on both wear resistance and toughness.
Corrosive plastic area
Consider corrosion-resistant mold steel such as S136.
This approach puts premium material where it provides the greatest return.
Practical Tool Steel Selection Workflow
For a glass-filled plastic injection mold, the following workflow is more reliable than selecting a grade based only on resin name.
Step 1: Identify the Polymer
Determine:
- Resin type
- Glass-fiber percentage
- Fiber length
- Additives
- Processing temperature
- Potentially corrosive components
A 15% glass-filled material and a highly reinforced engineering polymer should not automatically receive the same material recommendation.
Step 2: Identify the Failure Mode
Ask what is actually limiting mold life:
- Abrasive wear?
- Chipping?
- Cracking?
- Corrosion?
- Galling?
- Loss of polish?
- Dimensional change?
The failure mechanism should drive steel selection.
Step 3: Identify High-Wear Locations
Pay particular attention to:
- Gates
- Runners
- Core pins
- Thin ribs
- Shutoffs
- Slides
- Cavity corners
- High-flow regions
Step 4: Select the Steel Family
Consider:
- Conventional mold steel
- Cold work tool steel
- Toughened cold work steel
- PM tool steel
- Corrosion-resistant tool steel
Step 5: Define Heat Treatment
Specify:
- Target hardness
- Hardening process
- Tempering
- Stress relief
- Dimensional control
- Optional cryogenic treatment
Step 6: Evaluate Surface Treatment
If abrasive wear remains the dominant problem, consider:
- Nitriding
- PVD coating
- Other application-specific surface treatments
Step 7: Consider Replaceable Inserts
Do not automatically manufacture every component from premium steel.
Use premium material where the wear rate and replacement cost justify it.
Common Mistakes That Shorten Mold Life
Mistake 1: Using P20 for Severe Glass-Filled Applications
P20 and 718H are excellent general-purpose mold steels, but they may not provide sufficient wear resistance for extremely abrasive glass-filled compounds.
Mistake 2: Selecting Steel Only by Hardness
Hardness is important, but toughness, carbide structure and heat treatment are equally important.
Mistake 3: Ignoring Gate Wear
The gate may fail long before the main cavity.
Mistake 4: Overlooking Mold Geometry
Thin edges and small cores can fail through chipping rather than simple abrasive wear.
Mistake 5: Coating the Wrong Substrate
A PVD coating cannot compensate for an unsuitable or poorly heat-treated substrate.
Mistake 6: Ignoring Steel Quality
For demanding precision tooling, material cleanliness, carbide distribution and internal consistency can significantly affect service performance.
How to Reduce Cavity Erosion Beyond Steel Selection
Tool steel is only one part of the solution.
To reduce cavity erosion, mold engineers should also evaluate:
Injection speed
Excessive local melt velocity can increase abrasive action.
Gate design
Avoid unnecessarily concentrated flow through small or poorly positioned gates.
Mold surface finish
A suitable surface finish can help reduce local material accumulation and improve part release.
Cooling design
Stable mold temperature can reduce thermal cycling and dimensional changes.
Mold maintenance
Inspect gates, shutoffs, ribs and core pins before wear becomes visible on molded parts.
Replaceable wear inserts
Use replaceable components in areas with predictable high wear.
A complete solution normally combines material selection + mold design + processing optimization + preventive maintenance.
Tool Steel Selection by Application Severity
| Application | Recommended Direction |
|---|---|
| Low glass content, moderate volume | P20 / 718H or similar mold steel |
| Moderate glass-fiber content | S136, H13/SKD61 or wear-resistant mold steel depending on requirements |
| High glass-fiber content | D2/SKD11 or tougher high-wear tool steel |
| Severe abrasive wear | Premium cold work or PM tool steel |
| High-volume precision molding | Premium refined tool steel + optimized heat treatment |
| Severe local gate wear | Replaceable wear-resistant insert |
| Wear + corrosion | Corrosion-resistant tool steel or engineered surface treatment |
| Wear + chipping | Tougher tool steel with controlled hardness |
These are starting points rather than universal prescriptions. The actual material should be selected from the polymer, geometry, production volume and observed failure mechanism.
How KUTU MOLD STEEL Supports High-Wear Mold Applications
For glass-filled plastic injection molds, material selection should consider more than simply the steel grade listed on a material certificate.
KUTU MOLD STEEL can support mold manufacturers and mold engineers with:
- Mold steel selection
- High-wear cavity and core materials
- ESR refined tool steel
- Custom heat treatment
- Precision cutting
- Gantry milling
- Grinding
- Forged tool steel components
- Application-specific material recommendations
For demanding glass-filled applications, the objective is to select a steel that provides the required combination of wear resistance, toughness, dimensional stability and machinability rather than maximizing one property alone.
FAQ: Tool Steel for Glass-Filled Plastic Injection Molds
What is the best tool steel for glass-filled plastic?
There is no single best grade. D2/SKD11, DC53, PM tool steels and other high-wear grades may be suitable depending on glass content, mold geometry, production volume and failure mode.
Does glass-filled plastic wear out mold steel faster?
Yes. Glass fibers are significantly more abrasive than many unfilled polymer systems and can accelerate wear at gates, runners, cavities, cores and other high-flow areas.
Is P20 suitable for glass-filled plastic?
P20 can be suitable for lower-wear applications, but it may wear too quickly in high-volume molding with heavily glass-filled engineering plastics. A more wear-resistant insert may be a better solution.
Is harder mold steel always better?
No. Excessive hardness can increase susceptibility to chipping or cracking in thin or highly stressed mold components. Wear resistance must be balanced with toughness.
Can PVD coating prevent cavity erosion?
PVD coatings can improve surface wear resistance, but they cannot compensate for an unsuitable substrate, poor heat treatment or problematic mold design.
When should PM tool steel be considered?
PM tool steel becomes attractive when abrasive wear is severe, production volume is high, dimensional stability is critical or conventional tool steels cannot provide an acceptable maintenance interval.
Should the entire mold be made from premium tool steel?
Not necessarily. A hybrid design using premium steel only in high-wear cavity inserts, gates or cores can reduce tooling cost while maintaining wear resistance where it matters most.
Conclusion
Glass-filled plastic injection molding creates a more demanding environment for mold steel because glass fibers can produce aggressive abrasive wear during repeated high-pressure material flow.
The most effective way to stop cavity erosion is not simply to select the hardest steel.
A reliable strategy combines:
Wear-resistant tool steel + appropriate toughness + controlled heat treatment + optimized mold design + targeted surface treatment + replaceable wear components.
For high-volume and precision molding, premium refined tool steel can provide additional value when the cost of cavity wear, dimensional drift and mold downtime is significant.
If you are experiencing cavity erosion, gate wear, core wear or premature mold failure with glass-filled plastics, KUTU MOLD STEEL can help evaluate the application and recommend a suitable tool steel grade, heat-treatment condition and material-processing solution.
718H Pre-Hardened Plastic Mold Steel Plate | Precision 6-Face Milled P20+Ni Stock – KUTU
AISI P20 Pre-Hardened Plastic Mold Steel Plate | Precision Machined Mold Base Stock – KUTU
DC53 High Toughness Cold Work Die Steel Plate | Precision Machined Upgraded D2 Stock – KUTU
JIS SKD61 Hot Work Die Casting Steel Block | Precision Machined & Squared Stock – KUTU
JIS SKD11 Standard High Wear Hardware Mold Steel Plate | 6-Face Precision Milled Stock – KUTU