The Mold Was Already Using S136. So Why Change It?
A medical mold manufacturer came to us with a problem that was not unusual.
They were already using standard S136 for a high-gloss medical component. Corrosion was under control, and the material could achieve a good mirror finish.
But the customer wanted more.
The cavity needed a very high surface finish, the mold would run for long production cycles, and the polishing team was spending too much time correcting small surface imperfections.
The question was not whether S136 was a good mold steel.
It was.
The question was whether the particular S136 material and condition being used gave enough hardness, cleanliness and polishing consistency for this cavity.
For the replacement inserts, we discussed FT64, a 4Cr13 / 1.2083 stainless mold steel commonly positioned as an S136-equivalent grade.
After heat treatment, FT64 can reach around 50 HRC, while its combination of corrosion resistance, wear resistance and polishing performance makes it suitable for transparent and high-gloss plastic molds.
That difference matters when the cavity is not simply required to look good on the first trial, but to keep its surface quality through production.
Why Would an Engineer Move from S136 to FT64?
If a mold is already running well with S136, there is no reason to change steel just for the sake of changing it.
The situation is different when you start seeing problems such as:
- polishing takes too long
- small pits appear during final polishing
- cavity surfaces need repeated correction
- wear becomes noticeable after long production
- the customer wants higher hardness
- corrosion resistance is still required
FT64 is interesting because it keeps the basic advantages engineers look for in this family of stainless mold steels.
Its typical composition contains approximately 0.34–0.40% carbon and 13–14% chromium, depending on the specification. The chromium level provides the corrosion-resistant character expected from a 4Cr13/S136-type mold steel.
After hardening and tempering, published FT64 data commonly gives a hardness around 50 HRC.
That puts the material in a useful range for high-gloss cavities where surface wear and polish retention matter.
The Real Difference Shows Up at the Polishing Bench
This is where a steel specification becomes a production issue.
A cavity can be machined accurately and still become difficult during final polishing.
At a high-gloss level, the polisher is no longer just removing machining marks. They are trying to create a very uniform surface across the entire cavity.
If the steel has local inclusions, uneven structure or poor polishing behavior, the defects can become visible only near the end of the process.
FT64 is specifically marketed for high-polish and mirror-finish plastic molds, including transparent plastic products.
For a medical cavity, that matters because polishing time is not the only issue.
Every additional correction means:
more labor → more material removal → more risk of changing the cavity geometry.
That is why experienced moldmakers usually care about the steel’s polishing behavior before the cavity ever reaches the polishing room.
Higher Hardness Is Useful—But Only When You Actually Need It
This is another place where mold steel selection is often oversimplified.
More hardness is not automatically better.
For a high-gloss medical mold, you still need a reasonable balance between:
hardness + toughness + corrosion resistance + polishability + dimensional stability.
FT64 can be supplied in an annealed condition around ≤235 HB, and after the appropriate hardening and tempering process, published data gives approximately 50 HRC.
That hardened condition can provide better resistance to surface wear than a softer mold steel.
For a cavity that is polished repeatedly or exposed to long production cycles, that can become important.
But the correct hardness should still be determined from the cavity geometry, insert thickness, production conditions and heat-treatment specification—not simply from the highest number available.
A Practical Example: High-Gloss Medical Housing
Consider a transparent medical housing with a polished cavity surface.
The first mold uses conventional S136.
The mold runs correctly, but after extended production the customer starts seeing more frequent polishing maintenance. The cavity itself has not failed, but maintaining the original gloss takes more time.
For the next insert, the engineering team changes to FT64 and specifies the required hardness after heat treatment.
The objective is not simply to make the cavity harder.
The objective is to create a more stable combination of:
corrosion resistance + wear resistance + polishing performance.
That is a much more realistic reason to consider FT64.
And it is also why FT64 should not be sold as a universal replacement for S136.
If the existing S136 already meets the polishing, corrosion and wear requirements, changing material may provide little practical benefit.
FT64 vs. Standard S136: What Should Engineers Compare?
| Requirement | Standard S136 | FT64 |
|---|---|---|
| Stainless mold steel | Yes | Yes |
| S136-equivalent family | — | 4Cr13 / 1.2083 / 420 |
| Corrosion resistance | High | High |
| Mirror polishing | Very good | Very good |
| Typical hardened hardness | Depends on grade/process | Around 50 HRC in published FT64 data |
| High-gloss molds | Suitable | Suitable |
| Transparent plastic molds | Suitable | Suitable |
| Medical cavity inserts | Suitable | Suitable |
| Main reason to consider FT64 | Established stainless mold grade | Alternative grade with specific hardness/polishing requirements |
The key point is that FT64 should be evaluated by actual mill quality, heat-treatment condition and inspection data, not simply by the name of the grade.
Different S136-equivalent materials can behave differently depending on steelmaking route, cleanliness, forging, heat treatment and final condition.
When Does FT64 Make More Sense?
If you are making:
- transparent medical components
- high-gloss medical housings
- optical plastic parts
- precision cosmetic packaging
- corrosive plastic molds
- cavities requiring repeated polishing
FT64 is worth evaluating.
It becomes especially interesting when your current S136 solution is technically acceptable but you want to investigate:
higher working hardness, better wear resistance and more consistent high-polish performance.
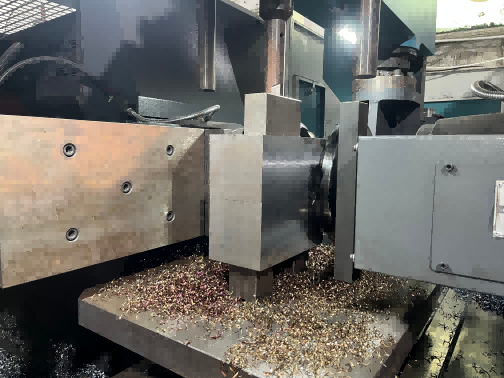
For demanding cavities, KUTU can also provide material inspection, cutting, precision machining and heat-treatment support rather than treating the steel block as a standalone commodity.
FT64 Mold Steel: Quick Engineering Answers
Is FT64 the same as S136?
FT64 is commonly identified with 4Cr13 / 1.2083 / AISI 420 / S136-equivalent material families. Exact chemistry and performance depend on the manufacturer’s specification, so the material certificate should always be checked.
Can FT64 reach 50 HRC?
Yes. Published FT64 processing data lists approximately 50 HRC after quenching and tempering. The actual result depends on section size and heat-treatment control.
Is FT64 suitable for mirror polishing?
Yes. FT64 is marketed for high-polish and mirror-finish plastic molds, including transparent plastic products.
Is FT64 better than S136?
There is no universal answer.
FT64 belongs to the same general stainless mold-steel family as S136, so the useful comparison is not simply “which grade is better?” It should be based on actual chemical composition, steel cleanliness, hardness, polishing requirement, corrosion exposure and production volume.
Why would a medical mold use FT64?
Because the application may require a combination of corrosion resistance, high hardness, wear resistance and mirror polishing. FT64 is specifically used for transparent plastic molds and molds operating in corrosive environments.
What hardness should I specify?
Do not specify hardness simply because “higher is better.” For a medical cavity, the target should be selected according to cavity geometry, insert size, toughness requirements, polishing requirements and expected production volume.
The Practical Takeaway
If your current S136 mold is already working, FT64 is not automatically an upgrade.
But if your next medical mold needs:
higher working hardness + corrosion resistance + high-gloss polishing + better wear resistance,
FT64 is worth putting on the material comparison list.
The important part is not the FT64 name itself.
Ask the steel supplier for the actual:
chemical composition, hardness, cleanliness, heat-treatment condition and inspection data.
That is what tells you whether the material is really suitable for the cavity you are trying to build.
For high-gloss medical molds, the best steel is not necessarily the one with the most impressive specification sheet.
It is the one that gives the polishing team a clean, stable material to work with—and keeps the cavity surface stable after the mold goes into production.
FT64 Mirror Polishing Plastic Mold Steel Plate | Precision Ground S136 Premium Stock – KUTU
S136 / S136H Corrosion Resistant Stainless Mold Steel Plate | Precision Machined ESR Stock – KUTU